We offer for our customers all bending tooling solutions for hydraulic and electric press brakes of main bending tooling clamping systems in the world: punches and dies, hemming sets, stamps, punchholders, die holders, adapters (including adapters between different tooling systems), die inserts, radius tooling with standard lengths and sectional types with rich selection of standard types and possility to make any special tools under request of customer including the length of 6000-8000 mm in one piece.
We are able to assist the customer to recommend tooling according to his parts as well as to prepare the sequence or quotation for special shapes if necessary.
Possibility to store lots of standard positions of bending tools with the marking and cutting before shipment allows to provide good delivery time even for big orders. All our bending tools are produced in Italy with the use of CNC machinery and quality control during different stages of production. For bending tools only high quality steels C45 or 42CrMo4 are used. The precision grinding allows the best contact with the material. All our tooling pass the temperature treatment till 55/60 HRC for long life use and effective protection against damages.
Together with the tooling we can supply the .DXF model for quick import to the CNC-library of press brake.
Bending tools, tooling for press brakes
Our main supply of press brake tooling:
- Amada / Promecam tooling system
- Trumpf tooling system
- Beyeler - Bystronic tooling system
- WILA tooling system
- LVD tooling system
- Roller bending dies
- Special and customized press brake tooling according to the customer request
Continuous Production & fast availability
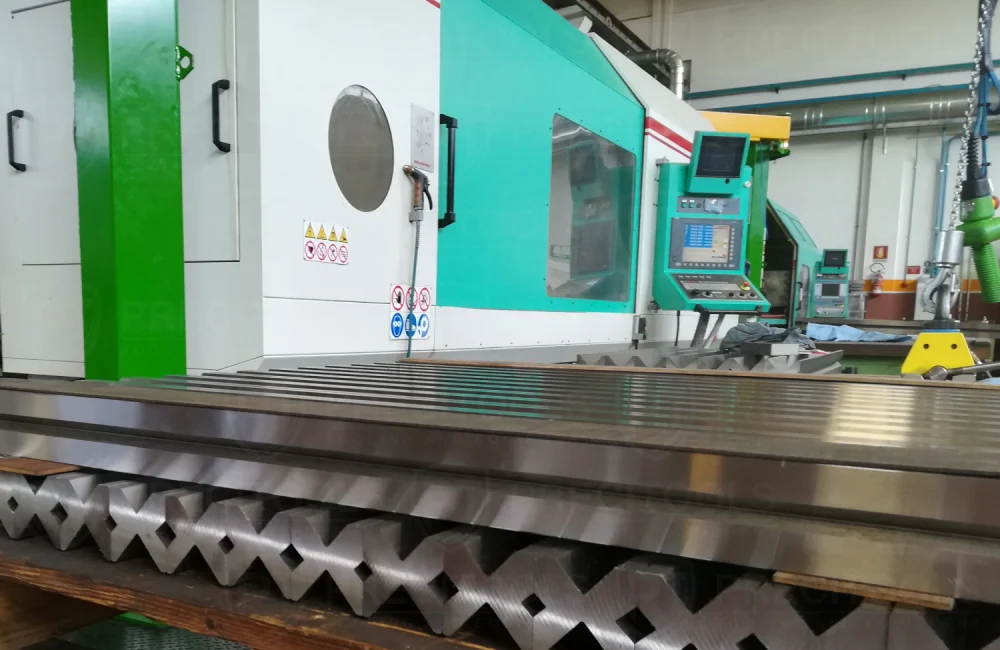
Our continuous production and stock of standard press brake tooling ensure that a wide range of commonly used items is available with short delivery times. This helps you avoid unnecessary delays and keep your production running without interruption. For subcontractors and sheet metal job shops, fast availability means the possibility to accept new orders and establish the required bending process in as little as one week.Our tooling is manufactured to high European standards, using European materials and precision machining and grinding processes to achieve tight and consistent tolerances. Consistent manufacturing quality also guarantees full compatibility from batch to batch. Even years after the original purchase, additional bending tools can be ordered and will fit seamlessly with the tooling already in use.
Not only bending tools
Thanks for wide cooperation with various manufacturers we are able not only to offer standard bending tooling positions for your press brake but complex solutions to make the parts which request normally stamping presses or punching presses. These could be actual for typical parts for stamping, busbars bending and forming, fabrication of electrical connector parts, brackets etc.- Forming tools for press brake
- Holes punching tooling
- Louvers forming
- Emboss, countersink and other forming punching operations
- Cutting
- Small flanges bending
- Bending near holes with minimal deformation
- Small radius bending
- Inserting
- Forming and stamping multiple parts in one stroke

Bending process visualization
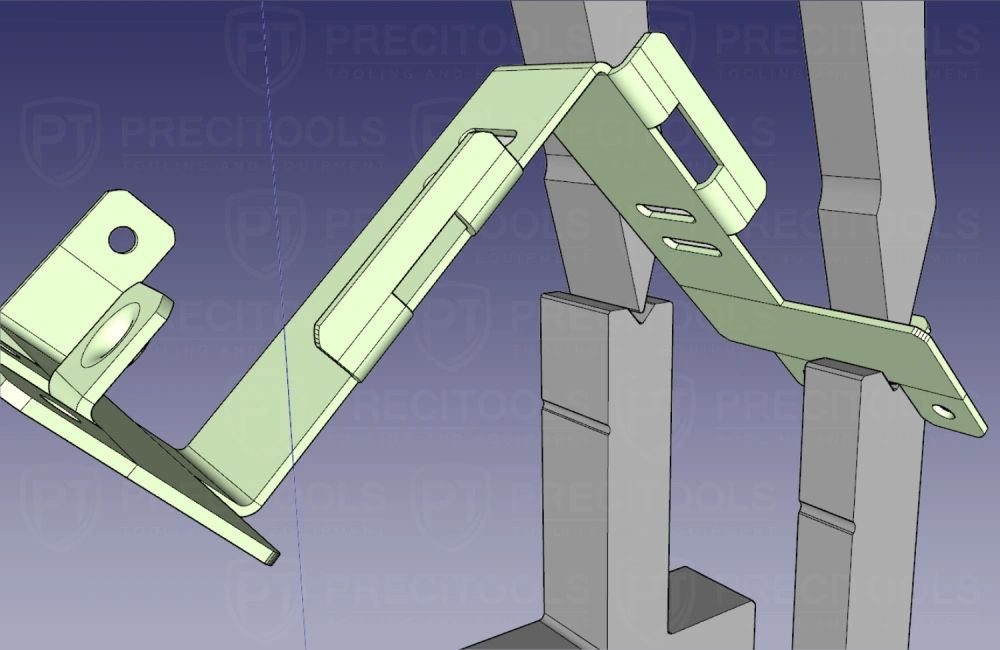
We use CAD-based bending visualization to precisely plan and validate the press brake bending process before production starts. By digitally defining the bending sequence, we can evaluate multiple setup options and eliminate the trial-and-error typically associated with manual planning. This results in smoother production launches, shorter lead times, and greater confidence that the part can be bent exactly as intended.
Our software allows us to determine the most efficient bending sequence, select the optimal punches and dies, and verify full machine compatibility. During the simulation, we perform detailed collision and clearance checks involving the part geometry, tooling, and, when necessary, press brake holders and other machine components. This helps identify potential issues early, including interferences and collisions.
For 1–2 parts requiring collision verification on the final bend, we are able to provide a detailed report within 24–48 working hours of receiving the parts. To minimize the risk of errors caused by springback, we perform the final bend based on the latest available springback / elastic return data.
For standard or symmetrical components, we typically prepare complete 2D drawings. For complex geometries or non-symmetrical shapes, we are also able to develop the entire project in a 3D environment.
Our experience, technological verification, and proposed solution enable the customer’s engineering and R&D teams to review and validate all relevant details before purchasing the bending tooling.
Our software allows us to determine the most efficient bending sequence, select the optimal punches and dies, and verify full machine compatibility. During the simulation, we perform detailed collision and clearance checks involving the part geometry, tooling, and, when necessary, press brake holders and other machine components. This helps identify potential issues early, including interferences and collisions.
For 1–2 parts requiring collision verification on the final bend, we are able to provide a detailed report within 24–48 working hours of receiving the parts. To minimize the risk of errors caused by springback, we perform the final bend based on the latest available springback / elastic return data.
For standard or symmetrical components, we typically prepare complete 2D drawings. For complex geometries or non-symmetrical shapes, we are also able to develop the entire project in a 3D environment.
Our experience, technological verification, and proposed solution enable the customer’s engineering and R&D teams to review and validate all relevant details before purchasing the bending tooling.